Matthias Surovcik
How a German facility assembling racks, cabinets, power conversion units and containerised storage systems can control stored energy and changing test states
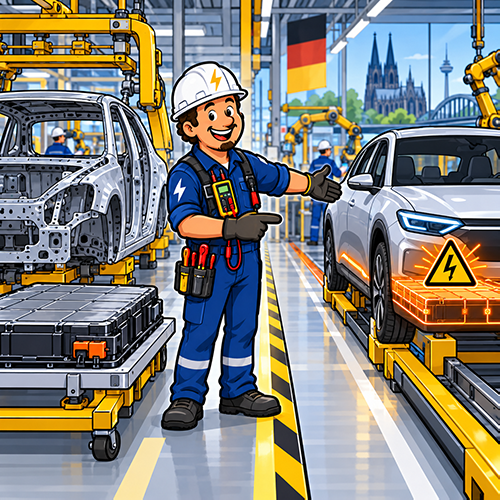
Your new plant receives finished cells or modules and assembles racks, cabinets and complete battery energy storage systems. It performs no electrode coating, electrolyte filling or cell formation. On the production plan, the facility therefore looks like an electrical assembly operation rather than a battery cell factory.
The distinction is correct, but it does not remove the electrical risk. Stored energy exists before the product is complete, fault energy rises as modules are connected, and test supplies or software commands can create new energy paths. The practical question is the electrical state at each workstation and what the assigned task can expose.
Map the product by energy state, not production department
A module in approved transport packaging has a different risk profile from an opened module under inspection. A cabinet with inhibited contactors differs from a system whose precharge circuit and battery management system are active.
For each state, the map should record nominal and maximum voltage, possible current sources, accessible conductive parts, stored energy, expected contactor position, discharge behaviour and the method used to verify the state. It should also show whether external power, an auxiliary supply, a charger, a power conversion system or a test set can energise the assembly. And please have in mind, it is not just the voltage-level that needs to be considered; it is the total risk assessment you have to take into account!
The map must include abnormal conditions. A dropped module, damaged connector, unexpected insulation value, welded contactor or lost communication cannot be managed by the normal production instruction. These conditions need a separate route to a controlled area with defined access, monitoring and technical escalation.
Convert the map into task specific competence
Electrical competence is not a general badge that applies to every battery task. Mechanical handling of a closed module, bolting exposed busbars, insulation testing, parameterising a battery management system and fault finding on an energised rack are materially different activities.
A task matrix should define the permitted activity, energy state, required competence, supervision, tools, personal protective equipment where needed and stop criteria. Repetitive work may be organised through engineered protection and a standard instruction. Work on an uncertain or live assembly requires a different assessment and may require a more highly qualified person and additional controls.
The production terminology must also be unambiguous. A display reading is not automatically proof of isolation. The verification method should address all sources, residual voltage and the possibility of remote or automatic reconnection.
Design the production zones around credible events
The physical layout should follow the energy states. Incoming inspection, ordinary assembly, electrical completion, live testing and quarantine need suitable separation. The level of separation depends on the hazards, not on a generic battery factory template. Access control, conductive work surfaces, tool selection, emergency isolation, signage and escape routes should match the activity performed in each zone.
Interfaces between battery racks, direct current buses, power conversion equipment, auxiliary supplies and test equipment require an isolation concept that identifies every source. Test connectors and temporary leads need ratings and protection appropriate to the prospective current.
IEC 62485 Part 5 addresses safety aspects associated with installation, use, inspection, maintenance and disposal of stationary lithium ion batteries. IEC 62933, Part 5, Section 2 addresses grid connected electrochemical energy storage as a system and the interactions between its subsystems. These standards provide relevant technical principles, but the production risk assessment must still reflect the unfinished product, the test arrangement and the work actually performed.
Control every transition
Each movement into a higher energy state should have a release condition. Before controls are enabled, software versions and interlocks are verified. Before dispatch, the final state, isolation, transport configuration and documentation are recorded.
Under the BetrSichV, the employer assesses hazards arising from work equipment, the working environment and the work object. The assessment should begin before equipment is selected and should include foreseeable faults. DGUV Regulation 3 applies to electrical installations and equipment used at the site. Product conformity and occupational control remain separate evidence streams.
Routine work remains efficient because task authority follows the energy state. Abnormal units leave the line, and each transition creates evidence for the next team.
Conclusion
The electrical risk in BESS assembly begins with credible exposure to stored energy, not with the factory label. For live testing, read “From Empty Test Bay to Energised Megawatt System”. Map every energy state before fixing the line layout, we are looking forward to your message (Click)
Frequently Asked Questions
Is a BESS assembly facility subject to the same controls as a cell factory?
Not automatically. Cell manufacture introduces chemical processes that may not exist in an integration facility. The BESS plant still needs a risk assessment for stored energy, exposed conductors, test sources, damaged units, electrical equipment and the interaction of complete subsystems.
When does ordinary assembly become electrical work?
The answer depends on the product state and task. Connecting conductors, accessing electrical parts, verifying absence of voltage or testing an energised assembly can create electrical work. The assessment should consider accessible voltage, energy, protective measures and credible faults.
Is opening battery contactors enough to make a rack safe?
Not by itself. The safe state must account for every source, stored charge, welded or incorrectly commanded contactors, auxiliary circuits and possible backfeed. The defined verification method should confirm the condition before work begins.
Which standard is most relevant to a stationary lithium ion battery installation?
IEC 62485 Part 5 addresses safety aspects of stationary lithium ion battery installations. For grid connected electrochemical storage systems, the IEC 62933 series adds system level considerations.
How should damaged or uncertain modules be handled?
They should leave the normal process through a predefined route. The site needs criteria for isolation, controlled storage, access, monitoring, emergency response and release or disposal based on manufacturer information and the risk assessment.